Industrial Sourcing Guide for 2177 Quality Parts
This guide explains how to evaluate and source 2177-grade components with a focus on quality control, supplier reliability, and pricing. It provides objective background on common procurement risks, inspection checkpoints, and documentation practices that help buyers make consistent decisions across vendors and shipments, without relying on unverified claims or fluctuating assumptions.
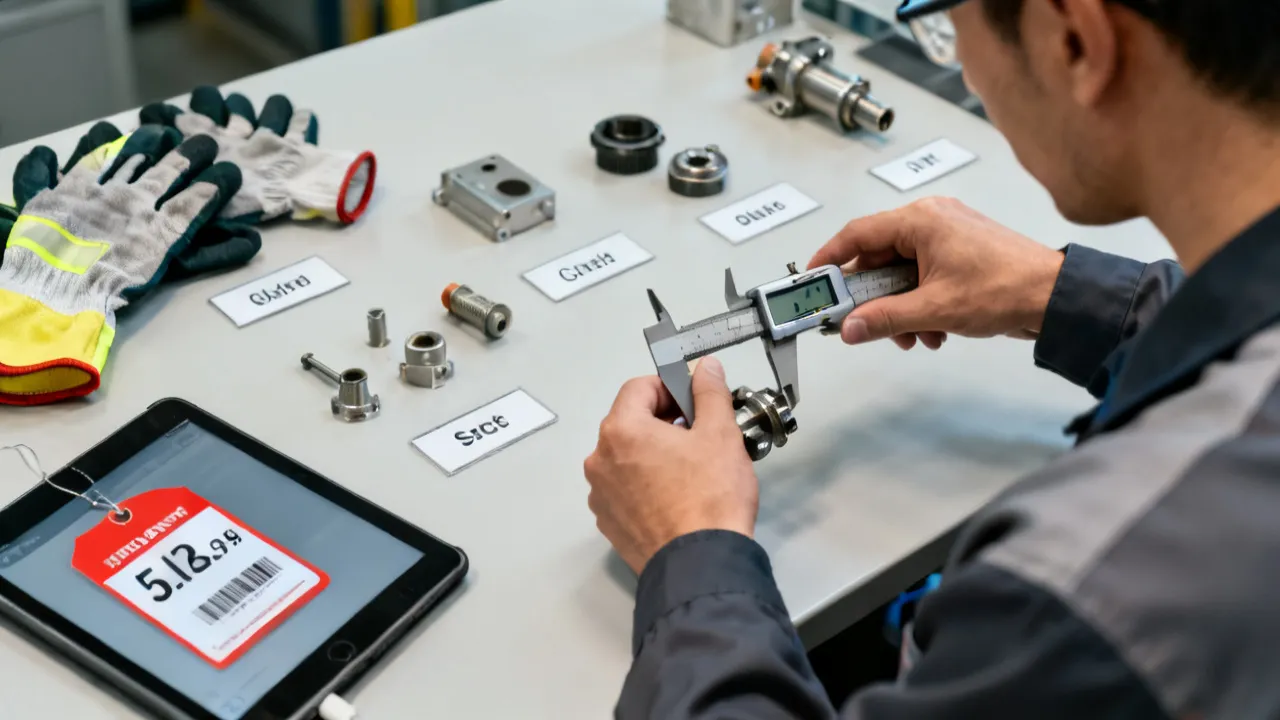
Critical first: how to approach sourcing “2177” parts with measurable quality
When you are sourcing parts identified as 2177 (including variations in model/grade codes used by different industries), your success depends less on the vendor’s marketing and more on your ability to verify quality through documentation, inspection, and standardized acceptance criteria. This guide focuses on practical, repeatable supplier evaluation—covering what to ask, how to compare offers that include price, and which supplier details matter when parts must perform reliably in production, maintenance, or regulated environments.
From an industry perspective, many sourcing failures come from treating “part number = identical part.” In reality, suppliers may use different tolerances, alternate materials, revision levels, calibration methods, or packaging standards—especially when the same short code (like 2177) is used across catalog sheets. To reduce risk, you should build your process around traceability, inspection evidence, and clear contract terms.
What “2177” typically signifies in procurement contexts
In procurement workflows, codes like 2177 often function as a shorthand identifier for a product line, spec revision, or a standardized internal reference. Depending on the sector—electrical components, industrial hardware, or component subassemblies—the code may map to:
- Design specification (dimensions, materials, performance limits)
- Manufacturing grade (tolerance bands, quality class)
- Revision level (changes in supplier tooling or process)
- Packaging or logistics configuration (anti-static, moisture control, labeling conventions)
Because the same “2177” label can be used differently by different suppliers, the buyer’s job is to confirm the full requirements—not only the code. A supplier may quote “2177” but fulfill it with a substitute that still “fits” physically yet differs in performance under load, temperature cycling, or lifespan expectations. Therefore, your evaluation should always begin by translating the code into measurable specifications.
To make this practical, you can treat every “2177” request as if it were missing one critical page: the page where the code is mapped to the detailed drawing, the revision number, and the test method used to verify the requirements. Your sourcing process should explicitly recover that “missing page” through paperwork, inspection, and contract controls.
Industry-standard evaluation: the “documentation + inspection + contract” model
To source 2177 components reliably, adopt a three-layer approach:
1) Documentation you should request
- Specification sheet tied to the exact revision
- Certificate(s) of Conformance (CoC) showing compliance to stated requirements
- Material declarations when applicable (e.g., for RoHS/REACH-relevant supply chains)
- Quality management evidence such as ISO 9001 certification status or an equivalent system description
- Traceability details (lot/batch numbers, manufacturing date codes, and backward trace links)
- Revision history or change notice (for any changes that occurred since your baseline)
- Calibration certificates when the supplier must certify that measurements were made against calibrated equipment (critical for dimensional, pressure, torque, or electrical test regimes)
Documentation should not be treated as a “set of PDFs.” It should be treated as a verification trail. If you have ever experienced a scenario where a CoC exists but does not mention the lot number or the measured parameters, you already know why this matters: documentation without linkage is simply paper, not proof.
2) Inspection evidence you should demand or schedule
- Incoming inspection plan aligned to your risk profile
- First Article Inspection (FAI) for new supplier onboarding or major revisions
- Sampling methodology (e.g., AQL-based sampling) agreed in advance
- Calibration references if the component or process requires measurement
- Process capability data (Cp/Cpk) for critical-to-quality dimensions/parameters when available, especially for high-volume orders
- Special process documentation where relevant (heat treat records, plating/finish process control, welding procedures/WPS/PQR for metal assemblies, etc.)
- Hold point strategy describing when the supplier “pauses” production to verify quality (e.g., at start of run, after tool changes, after maintenance)
Inspection evidence should be planned around what causes failure in the field or in your production line. For example, if a part’s failure mode is corrosion-related, you may need to validate coatings/finishes and packaging protection—not just dimensions. If failure mode is electrical overheating, you may need to validate resistive characteristics, insulation integrity, and workmanship standards.
3) Contract terms that prevent ambiguity
- Defined acceptance criteria (pass/fail thresholds, test methods)
- Revision control specifying “no substitution without written approval”
- Return/replace conditions (timelines, shipping responsibility, RMA process)
- Right-to-audit clauses where risk warrants it
- Communication requirements (nonconformance notification timelines, change notification timelines)
- Responsibility for rework (who pays when failures are traced to supplier-caused variation)
- Contingency handling (how you treat partial shipments, mixed-lot scenarios, or label mismatches)
This combination helps buyers compare offers with price that truly correspond to the same spec level, instead of assuming that a lower quote reflects an equal standard.
Understanding price: comparing offers without making assumptions
Pricing for 2177 parts typically varies due to yield rates, process controls, material sourcing, testing costs, packaging requirements, and order quantities. To compare quotations objectively, separate the commercial terms into categories:
- Unit price for your target quantity (and any price breaks)
- Testing and inspection costs included or excluded
- Lead time and whether expedited options exist
- Packaging standards (anti-static, moisture barrier, labeling)
- Documentation package costs (CoC/traceability/FAI reports)
- Logistics including incoterms and shipping method
- Fees for special handling (e.g., temperature monitoring, serialized labeling)
- Costs for compliance (RoHS/REACH documentation, test reports, material traceability)
As an industry expert would emphasize, “lowest unit price” rarely wins when you include total cost of quality. A slightly higher vendor price may be justified if it reduces the likelihood of rework, downtime, or acceptance failures.
To make price comparisons measurable, use a “total deliverable cost” concept. Not every supplier includes the same deliverables in a quote. For example:
- One supplier may quote unit price including CoC and lot traceability, while another quotes unit price but excludes those documents until after shipment (or provides them only for accepted lots).
- One supplier may include packaging that protects against moisture/ESD, while another provides basic packaging that increases latent defect risk.
- One supplier may provide test results for critical parameters, while another provides generic compliance statements.
Your procurement team should require quotes structured with line items for deliverables, so that differences in cost reflect differences in what you’re actually buying.
Supplier details that deserve real scrutiny
When evaluating supplier details, you should focus on operational reliability and quality governance, not only responsiveness. Key supplier evaluation factors include:
- Manufacturing footprint and process maturity (process controls, measured scrap/yield approach)
- Traceability capability (can they link each lot to production records?)
- Quality system scope (does their QMS cover the exact product family?)
- Communication quality (clarity in part revision matching, documentation format)
- Change notification practices (how they manage engineering changes)
- Corrective action performance (how they respond to nonconformities)
- Supplier qualification history (evidence that they have passed onboarding for similar products or in similar industries)
- Special process control (if coatings, plating, adhesives, welding, heat treat, or specialized finishing are involved)
- Statistical quality approach (control plans, in-process checks, use of SPC for critical characteristics)
Even when the quotation includes “2177,” a reputable supplier should readily map that code to a revision and provide the evidence needed to verify it. If the supplier cannot explain the revision logic or provide traceability artifacts, your risk increases.
One practical tactic is to ask for a “traceability sample.” Instead of requesting generic “traceability,” you can ask: “Provide a sample traceability report for the exact revision of 2177 you intend to ship, showing how lot/batch maps to your manufacturing traveler/records.” A supplier that can provide this quickly and clearly is signaling that they can support controlled production and containment if issues arise.
Risk management: common failure modes when sourcing coded parts
In real procurement programs, the following issues frequently cause delays and disputes:
- Spec drift: a vendor treats the code as “catalog only,” not revision-controlled
- Substitution without notice: alternate materials or processes used when supply constraints occur
- Testing mismatch: buyers test under one method while the supplier certifies under another
- Insufficient packaging: ESD/moisture exposure creates latent defects
- Document quality gaps: CoC exists but lacks lot mapping or measurement evidence
- Mixed-lot shipments: packaging or labeling errors result in mixed revision/lot arriving together
- Parameter ambiguity: the supplier certifies compliance to “requirements” but does not state the actual measured values for critical parameters
- Over-reliance on certifications: supplier provides ISO/RoHS statements without showing how they control the specific critical characteristics of 2177
Mitigation is straightforward: specify acceptance criteria, align test methods, require traceability, and validate with an initial pilot buy.
However, mitigation must be operational. It’s not enough to say “we’ll inspect.” You need to define:
- What you will inspect (critical characteristics, workmanship checks, packaging checks)
- How you will inspect it (test method, instrument requirements, sample quantity)
- When you will inspect it (receipt timing, hold-and-release steps)
- What happens if it fails (containment, RMA steps, CAPA expectations)
Localized procurement practice: how teams typically execute near-by sourcing programs
Where “nearby” supplier coverage is part of your plan—whether for faster replenishment, reduced shipping complexity, or minimizing disruptions—teams often prioritize:
- Shorter lead times to stabilize line-side production
- Better handling consistency through predictable packaging and routing
- More accessible communication channels for quality issues
- On-site inspection options when risks justify it
Practically, “nearby” does not automatically mean “lower risk.” It can help speed up resolution, but quality still must be proven through documentation and inspections. The top programs combine speed with disciplined verification.
In near-by sourcing, the biggest temptation is to reduce inspection because “they’re local.” Instead, you should consider a balanced approach:
- Keep incoming inspection for critical characteristics at the beginning and after any supplier process change.
- Use smaller sampling once a supplier demonstrates stable performance over time.
- Perform focused “process verification” events such as witness audits or targeted factory visits during start-up or tooling changes.
This preserves the speed benefits of near-by sourcing while maintaining quality control.
Comparison table: recommended conditions for evaluating “2177” offers
The table below is designed to help you compare suppliers using consistent conditions—without relying on unverified claims. It is written as a checklist of requirements and outcomes you can enforce in your sourcing process.
| Evaluation condition | What you should require | How it affects sourcing decisions |
|---|---|---|
| Part identity verification | Exact revision mapping for the 2177 code; specification sheet matching that revision | Prevents substitution risk and spec drift |
| Traceability evidence | Lot/batch traceability and links to production records; labeling requirements | Enables controlled containment if defects appear |
| Price comparability | Breakdowns showing unit price, inspection/documentation inclusions, and shipping terms | Supports total cost of quality analysis |
| Quality system coverage | QMS scope relevant to the exact product family; audit history or certification documentation where applicable | Improves expectation of consistent process control |
| Inspection plan alignment | Agreed acceptance criteria and test methods; defined sampling approach | Reduces disputes at receiving |
| Nonconformance response | RMA procedure, replacement/credit terms, corrective action expectations | Limits operational downtime and recurring defects |
| Change notification policy | Written notification timeline and approval requirements for engineering changes | Protects good stability for production lines |
Step-by-step guide: onboarding and purchasing “2177” parts
Use the following steps to reduce sourcing risk and ensure your price quotations correspond to the right quality level for 2177 components.
-
Translate the code into a specification checklist
Convert “2177” into explicit requirements: dimensions, materials, performance metrics, tolerances, allowable test conditions, and documentation requirements.Include at least three categories in your checklist: (1) “critical to quality” performance metrics, (2) “critical to function” mechanical/electrical parameters, and (3) “critical to fit/assembly” characteristics that drive compatibility with your downstream process.
-
Request supplier documentation
Ask for the revision-linked spec sheet, CoC, traceability approach, and any relevant quality system documentation.Also request the supplier’s control plan for the specific revision. If the supplier has a documented plan for controlling critical characteristics (what they measure, how often they check, and what they do when values trend out of control), that is stronger evidence than a certification alone.
-
Normalize quotations
Require line-item pricing for unit price, testing/documentation inclusions, packaging, and shipping terms. This creates a fair comparison.If a supplier offers a low unit price but excludes packaging protection, treat that as a “hidden cost risk.” Either require the missing deliverables, or adjust your decision to reflect the additional inspection and risk mitigation you’ll need to apply internally.
-
Perform a pilot order
Place a small initial order from your shortlisted supplier(s) and run incoming inspection using the acceptance criteria you defined.Design the pilot order to test what can go wrong. If you’re worried about latent defects from packaging, ensure the pilot includes your normal storage and handling conditions (e.g., time in warehouse, exposure conditions, shelf life monitoring). If you’re worried about revision drift, require the supplier to ship only a single lot with clearly matching labels.
-
Hold a quality review
If results differ from expectations, request corrective action reports and root-cause explanations—do not simply renegotiate unit price.In quality reviews, focus on whether the supplier can prevent recurrence. Ask for CAPA details that connect root cause to corrective actions, verify controls, and timelines. Your goal is to determine if the issue is systemic or isolated.
-
Lock revision and contract terms
Once validated, add revision control, “no substitution” conditions, and nonconformance handling to your purchase agreement.Make revision control explicit. You may want to specify: “Supplier shall not ship any revision other than X.Y for code 2177 unless written approval is granted by Buyer QA/Engineering.” Also require change notification in advance of shipment (with dates and documentation format).
-
Establish ongoing verification
For production-scale orders, schedule periodic checks or statistical monitoring based on the criticality of the component.Ongoing verification should adapt. When performance is stable, you can reduce sampling frequency under controlled conditions. If performance degrades, revert to higher sampling or request additional documentation for each shipment.
Conditions and requirements for successful procurement governance
To ensure the process works across suppliers, align internal stakeholders (purchasing, quality, engineering, logistics) on the same set of requirements. In particular:
- Engineering owns the specification translation and test method alignment.
- Quality owns inspection criteria, sampling approach, and nonconformance reporting.
- Purchasing owns contract language, price comparability, and supplier performance tracking.
- Logistics ensures packaging and handling conditions are documented and consistently applied.
When teams are aligned, you can avoid common failure modes where purchasing agrees to a delivery but quality later cannot accept because documentation or test method doesn’t match. A simple governance document can help: a “2177 Sourcing Control Plan” that lists the required deliverables, inspection steps, and decision authorities.
Source notes (method and reliability)
This article’s procurement recommendations reflect widely used industrial quality management practices. For further context on commonly referenced quality system concepts, buyers often consult:
- ISO 9001 for quality management system foundations (process control, corrective action orientation).
- ISO 2859-1 and related sampling guidance for acceptance sampling practices (when AQL-style methods are used).
- IEC and industry safety/testing standards when the component falls under regulated technical test requirements.
Because your “2177” code may map to different product types, you should match the documentation and inspection strategy to the applicable standard(s) for your domain.
For example, in some electrical or electromechanical components, test standards and certification requirements can be legally and operationally significant. In those cases, you should ensure your acceptance criteria specify both the test method and the pass/fail thresholds exactly, so there is no room for interpretation.
Expanding your approach: building a “2177” specification-to-evidence mapping
One of the best ways to prevent disputes is to create a mapping document that links each specification requirement to a specific evidence artifact and an inspection method. Think of this as a traceability matrix for your own procurement verification process.
For each line item in your “2177 specification checklist,” define:
- Requirement: the exact parameter and tolerance/performance limit
- Evidence type: CoC, test report, material declaration, FAI report, dimensional inspection record, or process control record
- Evidence source: supplier document reference (title/date/revision) or your receiving inspection report
- Acceptance method: test method name/standard, instrument type/accuracy, sample size, and required conditions
- Escalation path: what triggers a nonconformance and how quickly you require response
This approach makes your quality control defensible. It also helps reduce “argument loops” during receiving because everyone can see exactly how a decision is made.
If you’re dealing with multiple suppliers for “2177,” the mapping also enables consistent evaluation across vendors: you can score suppliers against the same criteria and prevent one vendor from being compared using incomplete or different evidence sets.
Handling revision control and change management for “2177” over time
Revision mismatches are one of the most costly procurement failures for coded parts. Even if physical fit is identical, revision changes can affect performance, reliability, compliance, or compatibility with downstream assembly processes.
To manage this, treat revision control as a contractual and operational requirement—not a “best effort” promise. Practically, implement the following controls:
- Require revision mapping on the quote: suppliers should state which drawing/revision corresponds to “2177” and attach the revision-linked spec sheet.
- Lock revision in the purchase order: include revision identifiers directly on the PO line item so warehouse receiving can reject non-matching parts.
- Define labeling requirements: require lot/batch number labeling and a visible revision indicator where feasible. Where labeling is not feasible, require documentation that uniquely identifies revision.
- Mandate change notification: require written notification before shipments reflecting the new revision and require buyer approval for continued shipments.
- Require re-qualification thresholds: define in the contract what changes trigger re-qualification—new materials, process changes, tool changes, or changes in test methods.
In many organizations, revision control also needs internal discipline. If engineering updates documentation but purchasing does not update PO language, you can inadvertently accept parts that technically meet an older spec but not the current revision requirement.
Designing incoming inspection for “2177” parts: what to inspect and why
Incoming inspection is often treated as a generic “count and check.” For 2177 sourcing, you should design inspection around the most likely failure modes and the highest-risk parameters.
A robust incoming inspection plan should typically include:
- Verification of part identity: check revision/label, lot code, and packaging labeling against PO and shipping documents.
- Dimensional and workmanship checks: measure critical fit/function characteristics with defined instruments and accuracy requirements.
- Performance parameter checks: if the supplier does not already test or if the parameters are critical for your use case, perform receiving tests on sampled units.
- Packaging condition checks: assess ESD/moisture barriers, seal integrity, and labeling legibility. Even a perfect electrical part can fail if packaging causes corrosion or insulation degradation.
- Documentation review: confirm CoC completeness, traceability mapping, and test results consistency with accepted test methods.
When writing your acceptance criteria, avoid ambiguity. For each parameter, specify:
- Pass/fail thresholds
- Test method reference (standard or internal procedure)
- Sampling plan and acceptance number
- Instrument or measurement system requirements
- Environmental conditions required for testing (temperature/humidity/charging conditions/time-at-condition)
In regulated or safety-critical environments, incoming inspection may need to include witness tests or third-party confirmation. In those cases, your contracts and supplier onboarding should already reflect those requirements.
First Article Inspection (FAI) for “2177”: making it efficient and complete
FAI is often mandatory for new suppliers, major revisions, or after significant process/tooling changes. To avoid wasting effort, scope FAI to the parts and processes that matter most.
A practical FAI approach for “2177” typically includes:
- FAI plan referencing your specification checklist and your acceptance criteria
- Dimensional measurements for critical characteristics (with measurement method and calibration evidence)
- Functional/performance tests aligned with how your part must operate in production
- Material and process confirmations (e.g., plating/heat treat records, adhesive process records if applicable)
- Packaging and labeling verification to ensure warehouse and line handling won’t create defects
Efficiency comes from completeness and clarity. If you require FAI results but you do not define which characteristics are critical, you may receive extensive reports that still do not cover the parameters you actually need. Therefore, link the FAI scope to your “specification-to-evidence mapping” so your FAI deliverable directly supports acceptance decisions.
Sampling and acceptance: turning “inspection” into a controlled decision
Sampling plans should not be arbitrary. They must be justified by risk, criticality, and historical performance.
Common sampling-related questions you should answer early include:
- Are 2177 parts critical-to-safety or critical-to-function in your assembly?
- What failure rates or defect patterns have you seen historically (internal or from industry)?
- What is the cost of a false accept (passing bad parts) versus a false reject (rejecting good parts)?
- What is the expected process capability (if the supplier can share Cpk or similar metrics)?
- What is the cost/time impact of inspection and testing?
In high-risk situations, you may implement additional controls beyond sampling, such as 100% inspection for one or two critical parameters, or short-run verification testing until the supplier demonstrates stability.
Also, ensure the supplier understands that acceptance sampling does not replace traceability. Even when you sample, you still need lot/batch traceability so you can contain entire lots if the sampled units indicate problems.
Packaging, handling, and latent defect risk for “2177”
Packaging is often underestimated because it doesn’t show up in unit price comparisons. Yet it directly affects reliability. For “2177” parts, packaging requirements may include:
- ESD protection (anti-static bags, ESD foam, conductive labels)
- Moisture barrier (vacuum sealed bags, desiccant, humidity indicators, controlled shelf life)
- Correct labeling (revision, lot code, handling instructions)
- Durable transit protection (shock/impact protection when handling failure is likely)
- Conformance with storage conditions (e.g., recommended storage temperature/humidity and maximum exposure time outside packaging)
To control latent defect risk, you can add “packaging verification” to receiving inspection. For example, you can verify seal integrity, check humidity indicator status (if applicable), confirm presence of desiccant, and confirm packaging date codes. If packaging failure is possible, your acceptance criteria should include packaging as an inspection category—because a part can fail later due to what happened during shipping or warehouse storage.
Nonconformance handling for “2177”: contain, correct, prevent
Nonconformance handling should be defined before the first purchase order is issued. If a shipment fails acceptance testing, your team needs a clear path for containment, communication, and corrective actions.
In the contract and in your internal receiving procedures, define the following:
- Containment actions: stop-use/stop-line actions, quarantine rules, and labeling of suspect inventory
- Failure documentation: which test results and photos/reports you must gather to support nonconformance evidence
- RMA and replacement process: who issues RMA, timeline for supplier response, and shipment status handling
- Disposition rules: whether you will rework, scrap, return, or hold parts while investigating
- Corrective action expectations: root cause, corrective action, verification of effectiveness, and prevention actions
- Impact assessment: whether nonconforming parts might have already been used in assembly and what internal traceability actions must occur
- Cost recovery terms: define reimbursement for testing, scrapped inventory, expedited shipping, and downtime where applicable
To avoid slow resolution, set response time requirements. For example: supplier should acknowledge nonconformance within a defined number of business days, provide initial containment advice quickly, and submit corrective action documentation by a specified deadline.
Quality agreements and audit strategy: when to go beyond documentation
In many sourcing cases, documentation and receiving inspection are sufficient. But for critical applications, you may need a formal quality agreement and occasionally an audit.
Quality agreements for 2177 can include:
- Defined critical characteristics and acceptance criteria
- Change notification requirements
- Traceability requirements
- Right-to-audit clauses and audit frequency expectations
- Nonconformance reporting structure (format, timeline, and severity)
- Supplier performance reporting requirements (PPM, defect trends, corrective action effectiveness)
Audit strategy should be risk-based. If you have high downtime costs or failure consequences, audit earlier and more frequently. If the supplier has demonstrated stable performance, you can reduce audit frequency and increase targeted verification.
Creating an RFQ template for “2177” that reduces ambiguity
Procurement success often starts at the RFQ. If your RFQ is vague, you will receive quotes that are not comparable, and later you will struggle to enforce quality.
Below is a practical RFQ structure you can adapt for “2177” sourcing. Use it to require the evidence and deliverables you will enforce at receiving.
RFQ essentials:
- State: “Supplier shall provide parts identified as 2177 with revision mapping to the attached specification.”
- Require: “Provide revision-linked spec sheet and CoC for each shipment lot.”
- Require: “Provide lot/batch labeling and traceability documentation.”
- Require: “No substitution of materials/processes. Written approval required for any change.”
- Require: “Packaging must comply with specified ESD/moisture requirements.”
- Define: “Incoming inspection acceptance criteria include dimensional checks and packaging verification.”
- Define: “Supplier must support nonconformance with CAPA within defined timelines.”
Additional RFQ questions that improve supplier clarity:
- Which drawing/spec revision corresponds to “2177”?
- Do you maintain process control plans for critical characteristics? Provide an excerpt.
- What test method do you use for the critical functional parameters, and what standards reference those methods?
- Can you provide process capability data (if available) for those critical parameters?
- What packaging and storage conditions are used to meet reliability requirements?
- How do you manage engineering changes and change notification?
When your RFQ is strong, suppliers respond more consistently. That improves your ability to compare price and reduces post-award disputes.
FAQ expansion: deeper answers for “2177” sourcing
1) What does “2177” mean in a supplier quotation?
In procurement settings, “2177” is often an identifier for a product line, grade, or revision family, but the exact meaning can vary by supplier. You should request a revision-mapped specification sheet and confirm the measurable requirements behind the code. If the supplier can’t clearly connect “2177” to a revision-controlled specification and measurable parameters, treat it as a warning sign and clarify before ordering.
2) How should I compare price between suppliers offering the same “2177” code?
Compare normalized offers: unit price plus any costs for documentation, inspection/testing inclusions, packaging requirements, and logistics/incoterms. Then evaluate total cost of quality by considering expected acceptance yield, rework probability, and the cost of delays if acceptance failures occur. A useful technique is to compute an “effective delivered cost,” where you add estimated inspection costs, potential rework handling, and expected cost of defects based on supplier history or pilot buy results.
3) Do I really need a pilot order?
For a new supplier, a new revision, or any critical application, a pilot buy is a practical way to validate fit-to-spec and test-method alignment. It is especially useful when supplier documentation is incomplete or when “2177” might map to different revisions. The pilot should test the highest-risk dimensions/performance parameters, not just superficial fit.
4) What supplier details should I request first?
Start with revision-linked specifications, certificate(s) of conformance, and traceability (lot/batch labeling and records). Then request quality system scope evidence and a nonconformance/corrective action process. If special processes are involved, request process control evidence and any calibration or equipment validity records related to critical tests.
5) What acceptance criteria should be included in the contract?
Include defined pass/fail thresholds, the test method(s), sampling approach, required documentation, revision control language, and nonconformance handling terms (RMA, replacement/credit timing, and containment expectations). If your production environment is sensitive, include packaging and handling acceptance criteria as part of receiving inspection.
6) If suppliers are “nearby,” does that reduce quality risk?
“Nearby” logistics can reduce lead time and speed up resolution, but it does not remove quality risk. You still need verification via documentation and inspections, especially for latent defects or revision mismatches. In near-by sourcing, emphasize controlling substitutions and ensuring packaging protection during local warehouse handling as well.
7) How often should incoming inspection be performed?
The frequency depends on criticality, historical performance, and supplier stability. Many programs increase verification during onboarding and after changes, then reduce sampling if sustained quality results support it. A common approach is: 1) full documentation review each shipment, 2) receiving inspection sampling for critical parameters initially, and 3) adjust sampling frequency based on trend performance (while keeping packaging checks consistent).
8) Can I rely on a certificate of conformance alone?
Certificates are important, but they should not replace verification for critical parts. A combined approach—documentation review plus receiving inspection—gives better assurance and reduces disputes. Particularly for coded parts like “2177,” the key is whether the CoC is linked to the lot and whether it states measurable results for critical parameters.
9) What should I do if a shipment fails acceptance testing?
Initiate containment, document failures with test evidence, and require corrective action from the supplier. Apply the contract’s nonconformance terms for replacement/credit and decide whether to continue ordering after CAPA completion and re-validation (or after an agreed containment and risk assessment plan). Ensure you check if suspect parts were used internally and whether you need a controlled traceback investigation.
10) How do I ensure revision control for “2177” over time?
Require written change notification, specify revision mapping in the purchase agreement, and block substitutions without approval. For critical uses, require re-qualification if engineering changes occur. Internally, ensure PO line items reflect the correct revision and that receiving/warehouse staff are instructed to verify revision/label matching before release.
Closing perspective: consistent sourcing wins through verification, not assumptions
Whether your procurement program targets 2177 components through good contracts or “nearby” replenishment planning, the underlying principle remains the same: you must connect the code to measurable requirements, then confirm those requirements through evidence and disciplined acceptance criteria. When you do this, price becomes a meaningful comparison tool rather than a source of false confidence—and supplier selection becomes a structured process you can reproduce across projects.
If you share the industry context (e.g., electronics component, industrial hardware, or a specific application) and what “2177” refers to in your documents, I can tailor the inspection checklist, acceptance criteria structure, and RFQ wording to match your exact use case.
-

A Guide to Cost-Efficient Small Electric Cars for Seniors
-
Mastering Debt Consolidation: Boost Your Credit Score and Manage Interest Rates
-
Your Guide to Loans, Credit Checks, and Interest Rates
-
Affordable Independent Living: Finding the Right Senior Housing
-
Guide to Senior Living Apartments: Affordable and Comfortable Environments